

HDPE Pipe Jointing Machine: Step-by-Step Butt Fusion from Setup to Cooling
Butt fusion joins thermoplastic pipe ends by preparing them, heating them to the required condition and bringing them together under controlled force. On a pipeline, the difference between a strong joint and a rejected one usually comes down to the details: correct supports, clean fusion surfaces, a verified heater and a disciplined drag-pressure measurement. This step-by-step guide walks through the full HDPE pipe jointing process on a butt fusion machine, from setup and clamping to cooling and weld records. Always follow the approved project procedure and the machine manufacturer instructions.
The Sequence Is Simple; the Control Is Not
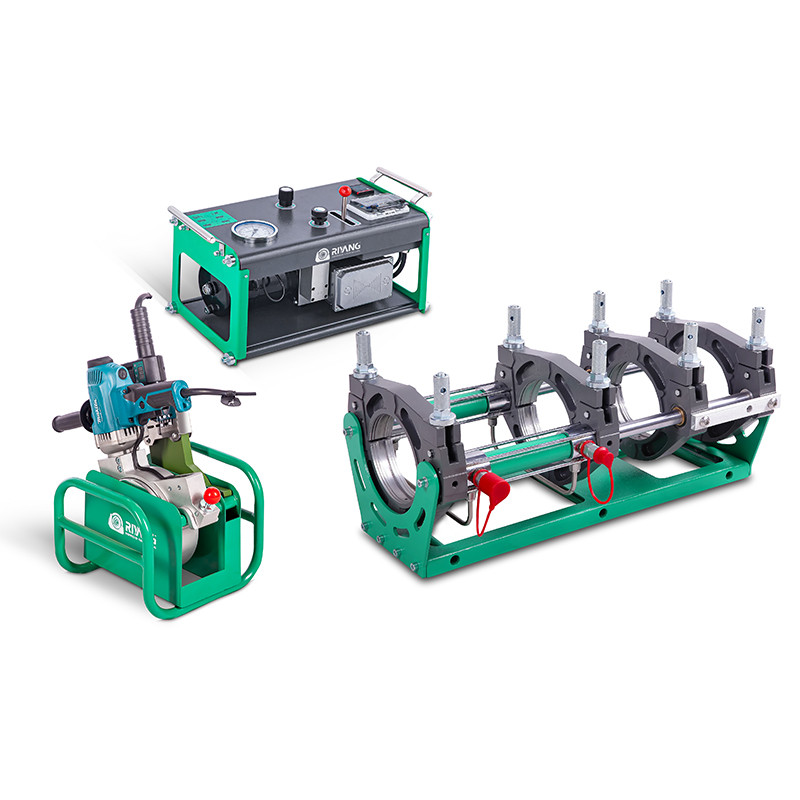
HDPE butt fusion follows a well-known sequence, but reliable joints depend on controlling alignment, heat, force and time at every stage. Skipping a single check — a contaminated fusion surface, an unverified heater or a stale drag-pressure reading — can produce a joint that looks acceptable but fails later. Work through the stages below in order and stop if the machine cannot hold the required temperature, pressure or alignment.
Step-by-Step Butt Fusion Procedure
Preparation and Setup
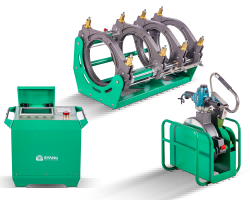
- Confirm pipe, procedure and equipment. Identify pipe material, OD, SDR and the applicable welding standard, then verify that the jointing machine, inserts, heater and facer cover the pipe size. Check calibration status, hydraulic oil, hoses, cables, heater surface and power supply before loading pipe.
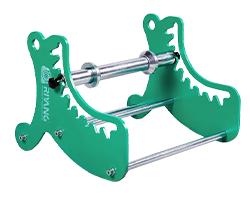
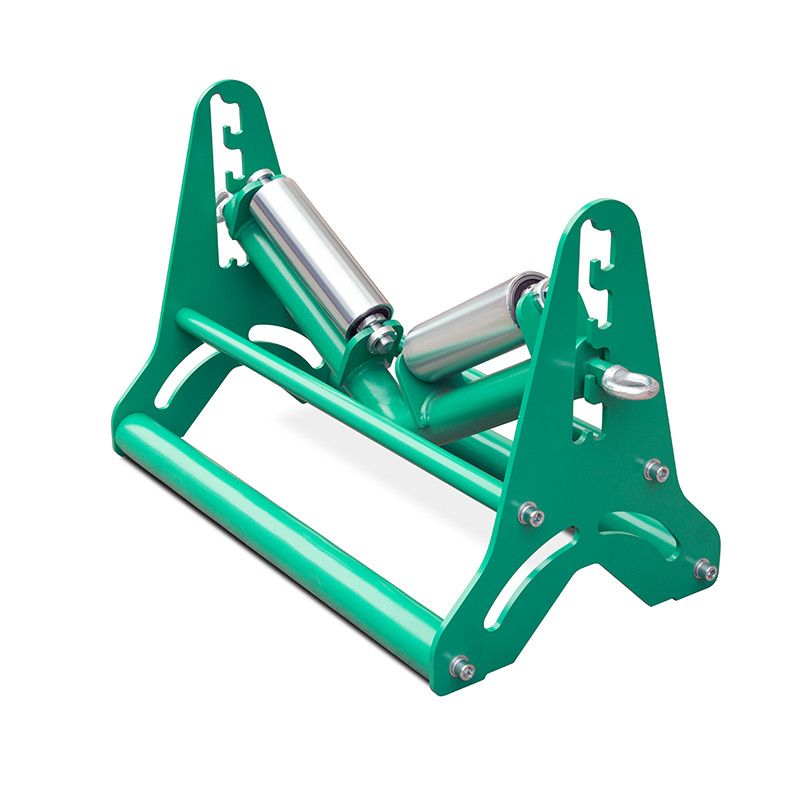
- Support and clamp the pipe. Position pipe supports or rollers so the pipe centerline matches the machine, clean the clamping area and install the correct inserts. Clamp securely while leaving enough material for facing; poor external support creates misalignment and excessive drag even on a correctly adjusted machine.

Face, Clean and Measure Drag
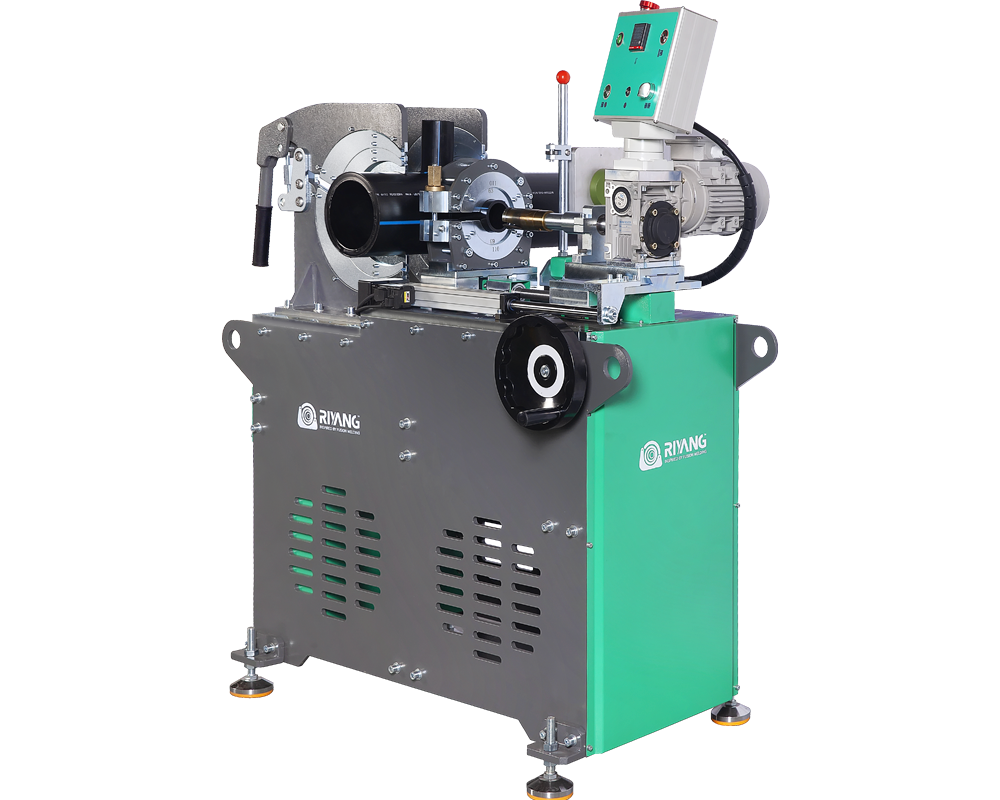
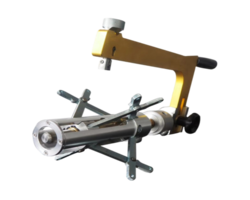
- Face both pipe ends. Insert the facer and bring the pipe ends into contact using the manufacturer procedure. Continue until both ends are clean and parallel and produce consistent shavings, then retract, stop and remove the facer safely and check alignment and gap.
- Clean without contaminating. After facing, do not touch the fusion surfaces with bare hands or dirty tools. Remove loose shavings without damaging the ends; if a prepared surface becomes contaminated, follow the approved procedure, which may require refacing.
- Measure drag pressure. On hydraulic machines, move the carriage and identify the pressure needed to overcome pipe and machine resistance. Drag changes with pipe length, slope, ground contact and roller arrangement, so re-measure whenever the setup changes.
Heat, Change Over and Fuse
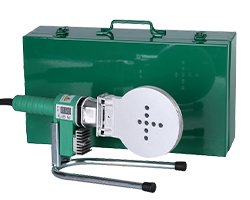
- Verify the heater. The heater must be clean, undamaged and stabilized at the temperature required by the approved procedure. A controller display alone does not prove the whole plate is uniform, so follow the project or manufacturer verification method.
- Bead-up and heat soak. Place the heater between the prepared ends and bring the pipe into contact according to the selected fusion procedure. The cycle may include a bead-up phase followed by a lower-pressure heat-soak phase — do not improvise times or pressures from another standard.
- Remove the heater within changeover time. Open the carriage, remove the heater without dragging it across the molten pipe ends, and close the carriage promptly. The molten surfaces begin cooling as soon as they leave the heater.
- Apply fusion pressure correctly. Increase to the required fusion pressure within the time allowed by the procedure, avoiding slamming the pipe ends together. The objective is controlled interfacial force and alignment, not maximum hydraulic pressure.
- Hold through the cooling period. Keep the joint clamped and under the required pressure for the specified cooling time, and protect it from rough handling until any additional cooling requirement is met.
Inspect and Record
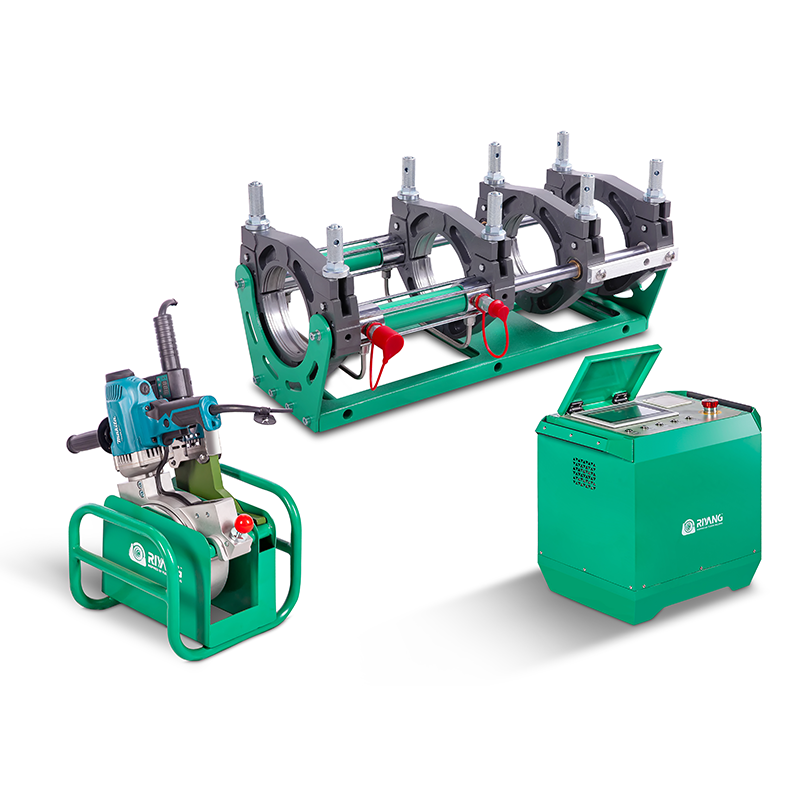
- Inspect and record. Check bead appearance and alignment against the applicable acceptance criteria, then record the joint identification and process data required by the project. Automatic equipment can help capture welding data, but the operator remains responsible for correct pipe preparation, setup and compliance with the approved procedure.
- Alignment — pipe supports, inserts, frame rigidity and coaxial loading
- Heat — heater cleanliness, temperature uniformity and stabilization
- Force — effective piston area, drag pressure and fusion pressure
- Time — heat soak, changeover and cooling hold
- Record — operator, project, pipe data, parameters and photos
| Phase | What to control | What goes wrong |
|---|---|---|
| Preparation | OD, SDR, inserts, calibration | Wrong inserts, unverified machine |
| Facing | Blade condition, parallel ends | Uneven or contaminated ends |
| Heating | Temperature uniformity, soak time | Cold spots, over or under soak |
| Fusion | Force, changeover time, alignment | Low interface force, misalignment |
| Cooling | Hold time, no early handling | Disturbed joint, weak interface |
Where Automation Helps
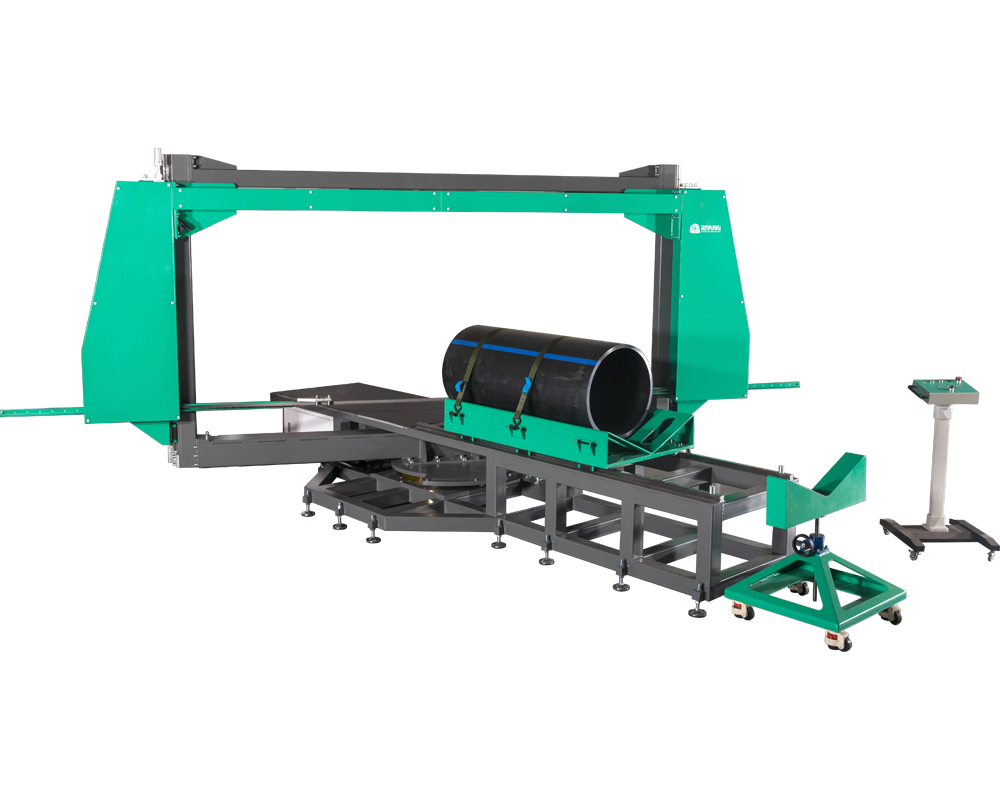
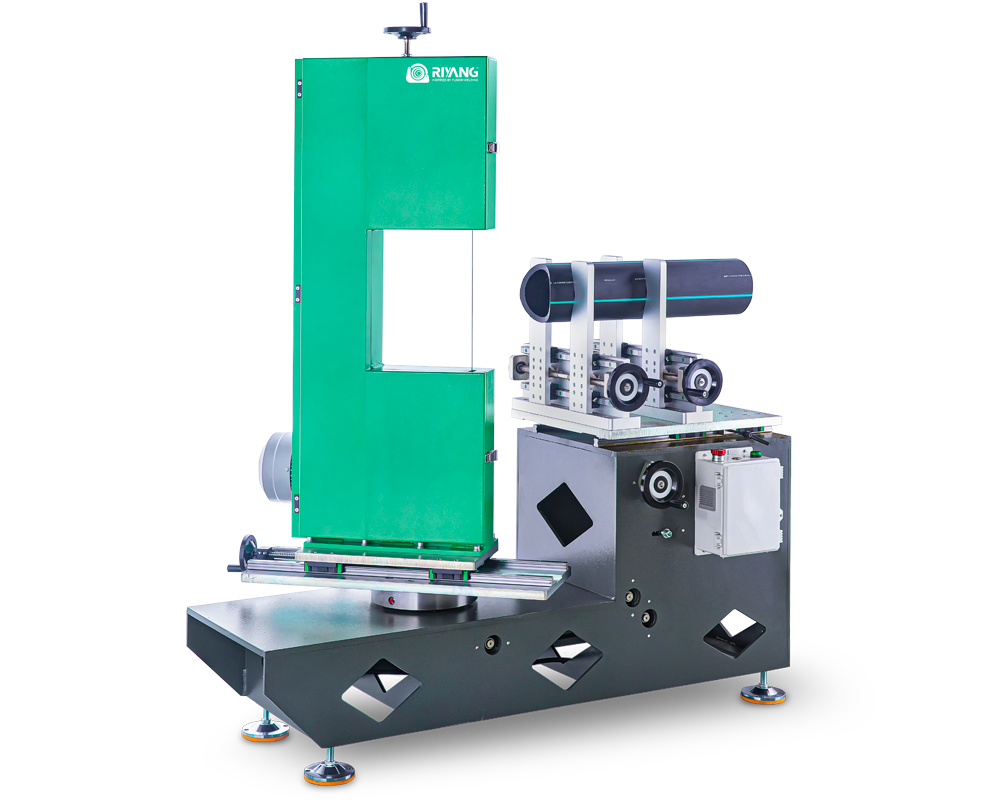
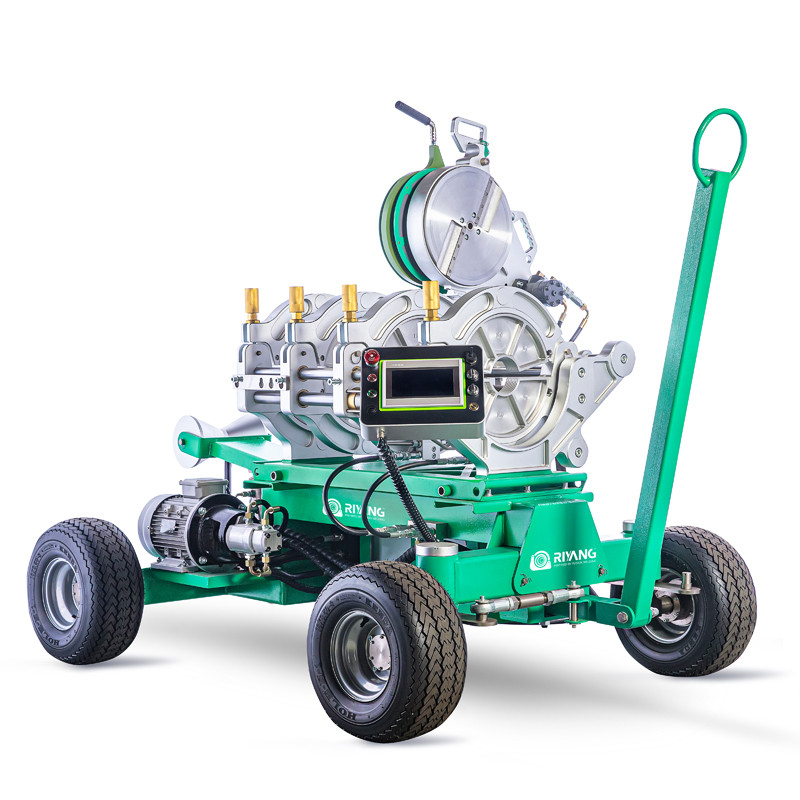
A CNC system can guide sequence, timing and pressure control and create a digital weld record, improving repeatability on projects with many joints or strict traceability. It does not remove the need for trained operators, clean pipe ends, correct supports or a suitable fusion procedure. When choosing equipment, start from the pipe and project requirements rather than a single headline specification — the RIYANG selection guide explains how OD, SDR, pressure class and jobsite conditions should drive the decision.
FAQ
What are the main steps in HDPE butt fusion?
The typical sequence is clamp, face, align, verify heater, heat, change over, fuse under controlled force, cool, inspect and record. Each step has acceptance criteria defined by the project procedure.
Why is drag pressure measured?
Drag pressure represents the resistance the hydraulic carriage must overcome. If it is ignored where the procedure requires compensation, the pipe interface may receive less force than intended and the joint can be under-fused.
Can I use one welding table for every project?
No. Use the procedure and parameters approved for the pipe, standard and project. Copying a pressure or time table from a previous job or another brand is a common cause of rejected joints.
Summary
Reliable HDPE pipe jointing is the product of a disciplined sequence: confirm the pipe and procedure, support and clamp correctly, face to clean parallel ends, measure drag pressure, verify the heater, heat and change over within the allowed time, apply the correct fusion pressure, hold through cooling, then inspect and record. For a project-specific welding table or machine recommendation, send RIYANG your pipe OD, SDR, material and the required fusion standard, or review the technical support FAQ for setup and diagnostic guidance.
Technical review by RIYANG Engineering Team.